

Robotic loading and unloading station solutions for automated consumer goods manufacturing.
20-03-2026 5
In consumer goods manufacturing plants, the packaging and palletizing of finished products is a crucial but often labor-intensive process, prone to errors, and impacting operational efficiency and production costs. A robotic palletizing station solution for the consumer goods industry fully automates this final stage, ensuring fast, accurate, and consistent palletizing.
The solution developed and synchronously integrated by Intech Robotics utilizes heavy-payload collaborative robots combined with advanced mechanical-control modules, suitable for various production models. Join Intech Robotics to explore the structure and distinctive benefits of this solution.
Structure of the Robotic Palletizing Station for the FMCG Industry
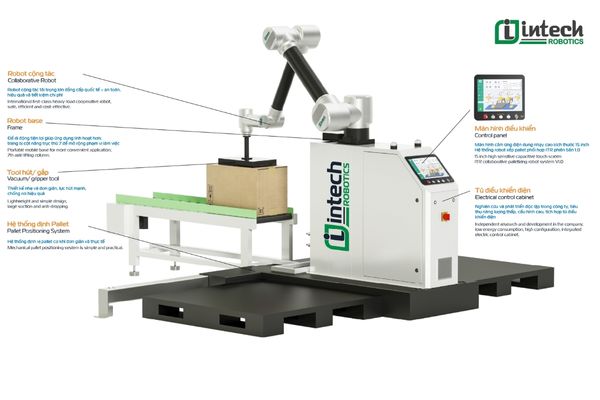
Heavy-Payload Collaborative Robot
The robotic palletizing station for the Fast-Moving Consumer Goods (FMCG) industry utilizes heavy-payload collaborative robots (Cobots) that meet international standards for safety and performance.
The robust mechanical structure and high rigidity allow the robot to stably handle packages, cartons, or product bags of light to medium weight. The system operates at optimal speeds while ensuring absolute safety when working near humans, meeting the modern production standards of the FMCG sector.
Mobile Base
The robotic station is designed with a mobile base, making it easy to move between production locations and reconfigure quickly when factory layouts change. This design helps businesses optimize space and enhance adaptability to fluctuations in output volume or product types.
7th Axis Lifting Column
Integrating a 7th-axis lifting column (Vertical Axis) allows the robot to move vertically smoothly and accurately, expanding the workspace according to pallet height. This enables the robot to efficiently handle various pallet stacking configurations, fitting the specific requirements of multi-layered and multi-sized consumer goods packaging.
Vacuum Suction Gripper
The station is equipped with specialized vacuum suction grippers optimized for cartons, packaging bags, or flexible packaging. Key advantages include lightweight design to reduce robot arm load, simple maintenance-friendly construction, stable grip, and minimized product deformation or drops.
Patented high-suction and anti-drop technology helps the robot maintain a stable grip even on uneven surfaces, ensuring absolute safety for consumer goods during high-speed palletizing processes.
Tag Positioning System
The robotic palletizing station integrates a Tag Positioning System that helps the robot accurately identify pallet positions and product placement points. This reduces deviations during stacking, increasing the precision, repeatability, and aesthetic quality of the palletized load. This simple yet durable mechanical positioning system is less dependent on environmental conditions, ensuring long-term stable operation.
Benefits of Applying the Robotic Palletizing Station Solution for the FMCG Industry
Simple Programming
The robotic palletizing solution is equipped with an intuitive Visual Programming interface, allowing users to easily set up stacking patterns without needing deep knowledge of complex programming languages.
Technicians can quickly configure pallet patterns according to order requirements, change box dimensions, adjust the number of layers, and flexibly modify stacking sequences.
Ease of Operation
The station supports various user-friendly control methods via a teaching pendant or remote controller, making adjustments easy for operators. The system is designed to suit production environments for products like wet wipes with diverse packaging, ensuring simple, intuitive, and easy-to-remember operations with rapid pallet configuration changes.
Safety and Stability
The station integrates force sensors and a multi-level collision detection mechanism (up to 10 levels), ensuring absolute safety for both operators and equipment.
Additionally, the system is equipped with comprehensive safety detection sensors and provides 16 safety I/O interfaces, maintaining stable operation even in the event of a single failure.
Flexible Design
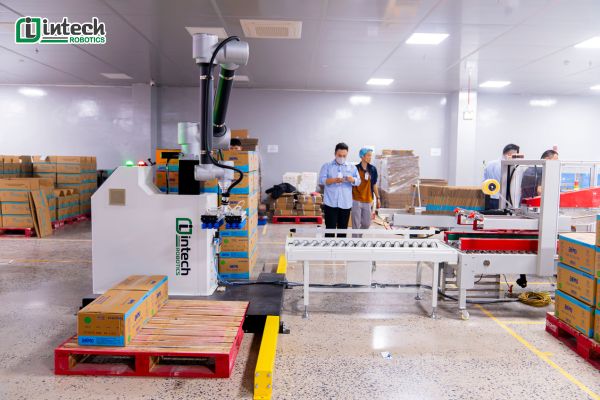
With its integrated and compact design, the robotic station is easily deployed at the end of packaging lines. Key benefits include rapid construction and installation, minimal floor space requirements, and suitability for factories with limited space or those looking to expand/renovate existing lines.
Flexible Production
The robotic station supports quick switching between multiple packaging scenarios, easily adapting to orders with diverse sizes and volumes.
The system can:
-
Facilitate safe human-robot collaboration.
-
Synchronously connect with case erectors, case sealers, and pallet stretch wrappers.
-
Operate multiple robots in parallel within the same line.
-
Integrate with AGVs/AMRs to form fully automated lines in the future.
Conclusion
The robotic palletizing station solution for the FMCG industry not only automates the final stage of the packaging line but also brings outstanding efficiency in productivity, precision, and operational safety. With flexible programming, ease of deployment, and synchronous integration with other automated equipment, the robotic station is a significant step forward in helping businesses reduce dependence on manual labor, optimize operating costs, and enhance product quality.
With experience in deploying hundreds of projects in robotics and automation, Intech Robotics is proud to partner with factories on the journey to building smart, flexible, and sustainable production lines.
